
Technical Specifications
A practical engineering reference for understanding knurl geometry, pitch systems, calculations, and pitch conversions.
On This Page
Tooth Form
A knurled tooth is V-shaped and the depth of the tooth is less than the depth of a theoretical V-form. The tooth has a rounded root and crest. The relationship between the actual depth of tooth to the theoretical V varies with the pitch of the teeth. On finer pitches, the tooth is a smaller proportion of the theoretical V-depth than coarser pitches. Also, female diamond patterns have shallower tooth depth than male diamond patterns.
RAPID offers 90° teeth angle as standard included pressure angle. As per customer requirement, RAPID manufactures custom teeth angles such as 80° and 60°.
Key Terminology
- Circular Axial Pitch
- Distance from tooth to tooth, in mm
- TPI (Teeth Per Inch)
- Number of teeth per linear inch, or 1" ÷ circular pitch
- Diametral Pitch (DP)
- Number of teeth on the work ÷ theoretical work blank diameter
Pitch Formulae
Axial pitch can be calculated from TPI or from Diametral Pitch (DP):
Where is axial pitch, is teeth per inch, and is diametral pitch.
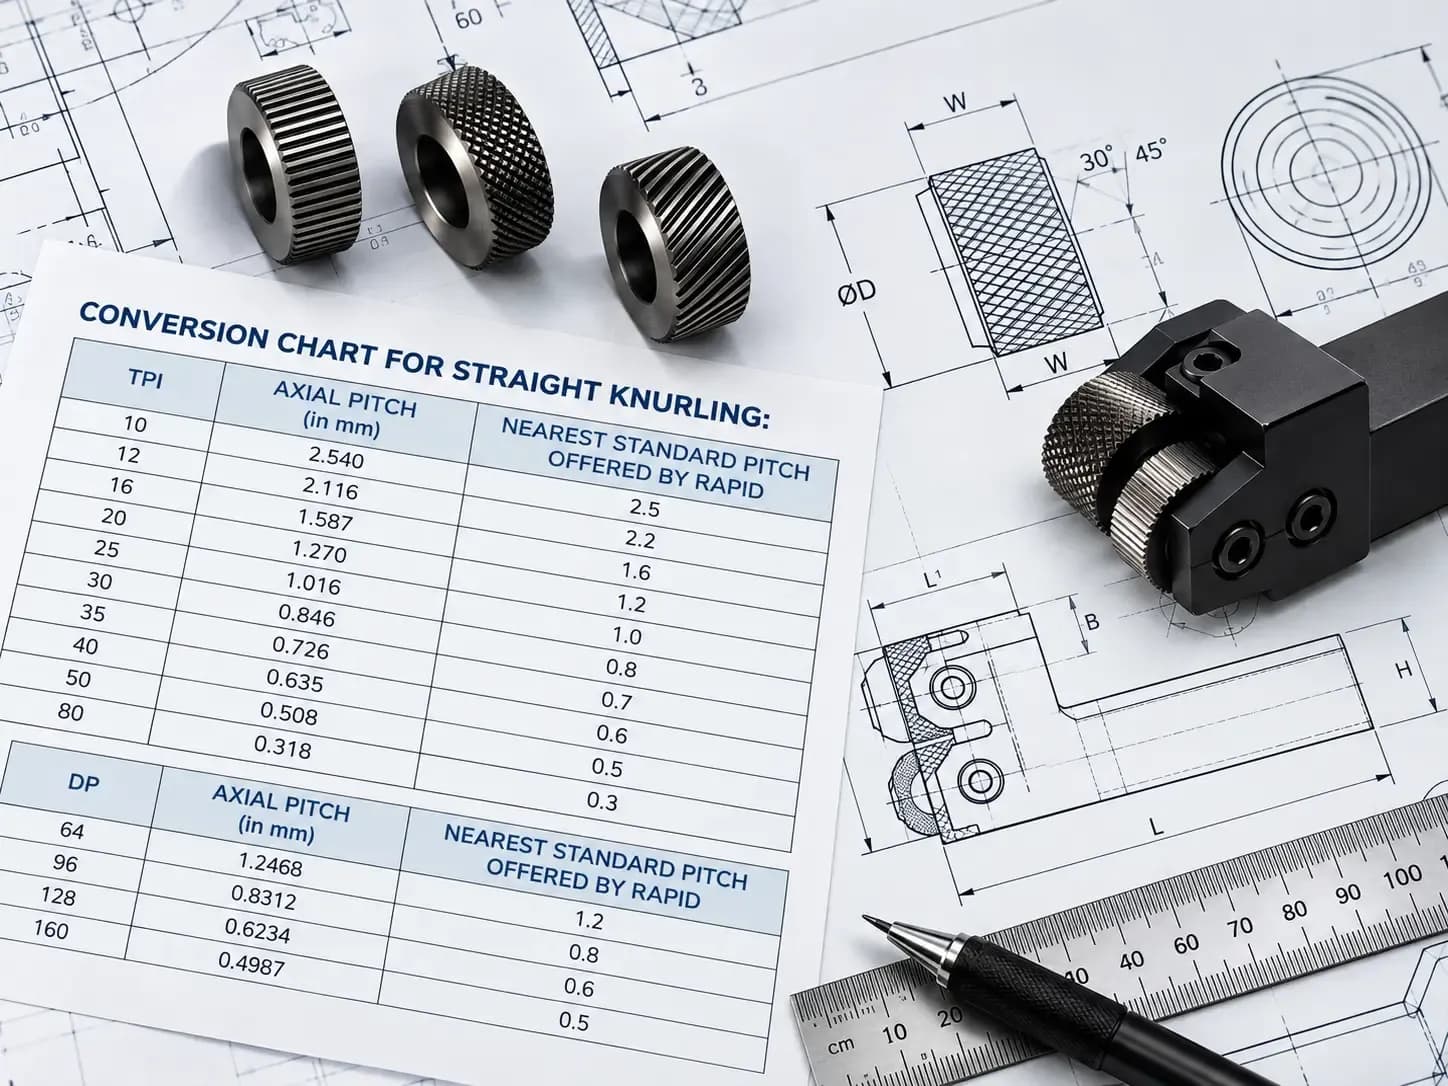
Conversion Chart for Straight Knurling
| TPI | Axial Pitch (mm) | Nearest Standard Pitch (RAPID) | DP | Axial Pitch (mm) | Nearest Standard Pitch (RAPID) | |
|---|---|---|---|---|---|---|
| 10 | 2.540 | 2.5 | 64 | 1.2468 | 1.2 | |
| 12 | 2.116 | 2.2 | 96 | 0.8312 | 0.8 | |
| 16 | 1.587 | 1.6 | 128 | 0.6234 | 0.6 | |
| 20 | 1.270 | 1.2 | 160 | 0.4987 | 0.5 | |
| 25 | 1.016 | 1.0 | ||||
| 30 | 0.846 | 0.8 | ||||
| 35 | 0.726 | 0.7 | ||||
| 40 | 0.635 | 0.6 | ||||
| 50 | 0.508 | 0.5 | ||||
| 80 | 0.318 | 0.3 |
Knurling Methods
In-Feed Knurling (Plunge) on CNC "X"
Straight or diamond knurling can be produced by using either one or two knurls mounted in a holder in the front or rear of the cross slide, which applies direct pressure to the work. Diamond knurls require greater pressure than straight or diagonal knurls, sometimes placing prohibitive loads on both machine and work, which can damage the machine.
End-Feed Knurling (To Chuck) on CNC "Z"
Straight, helical, or diamond knurling may be produced with knurling holders mounted on the compound or turret. Only straight and diagonal knurls can be used with the end-feed process; to produce helical and diamond knurling, the knurls are held in the holder to trace the helical or diamond path as they are fed over the blank.
Note: Knurls used for feed knurling should have chamfers.
Knurling Standard (IS: 3403-1981 & DIN82)
RAPID™ knurl patterns follow the profile and diameter standard defined in IS:3403-1981 and DIN82, at a standard 90° profile angle.
Pattern Types
| Code | Description |
|---|---|
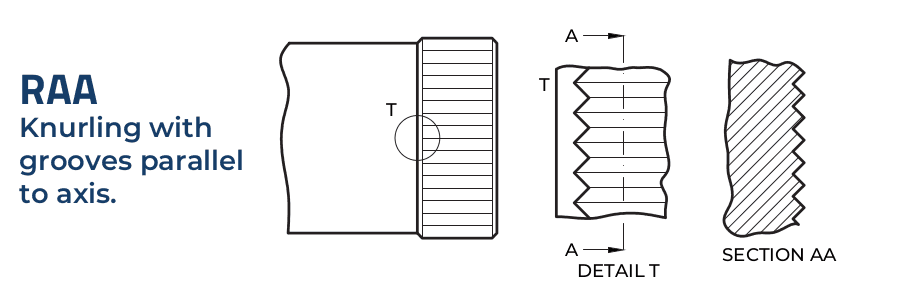
| RAA | Knurl with grooves parallel to axis |
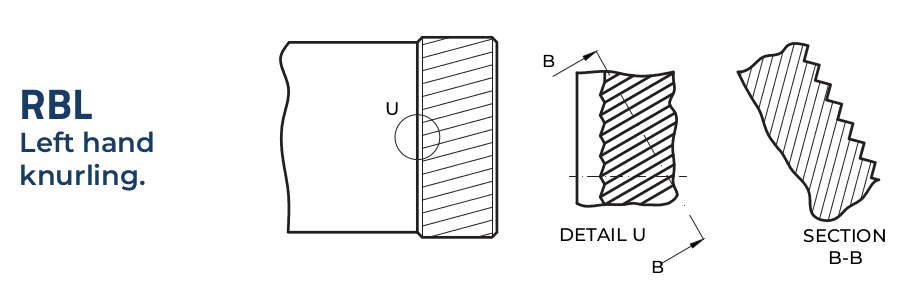
| RBL | Left-hand knurl |
| RBR | Right-hand knurl |
| RGE | Left-hand / right-hand knurl, points raised |
| RGV | Left-hand / right-hand knurl, points indented |
| RKE | Cross-knurl, points raised |
| RKV | Cross-knurl, points indented |
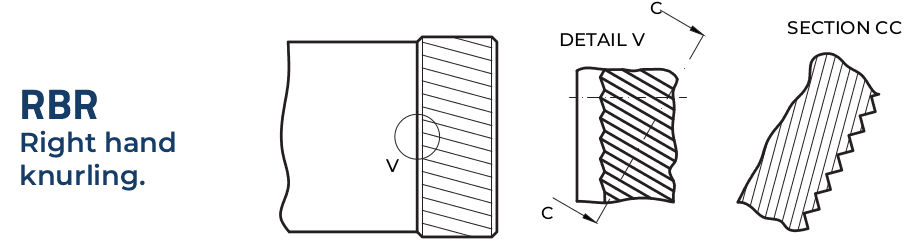
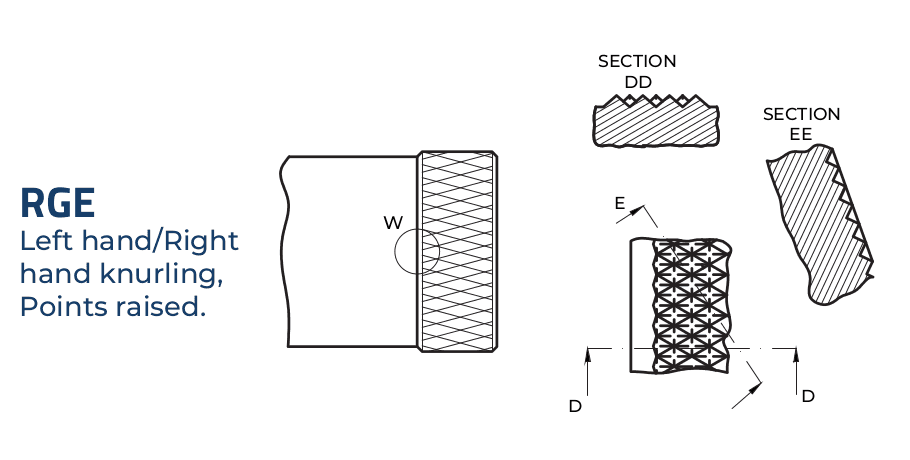
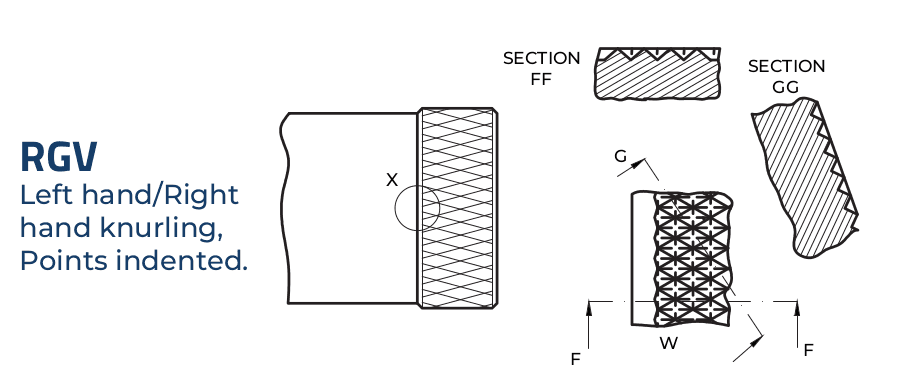
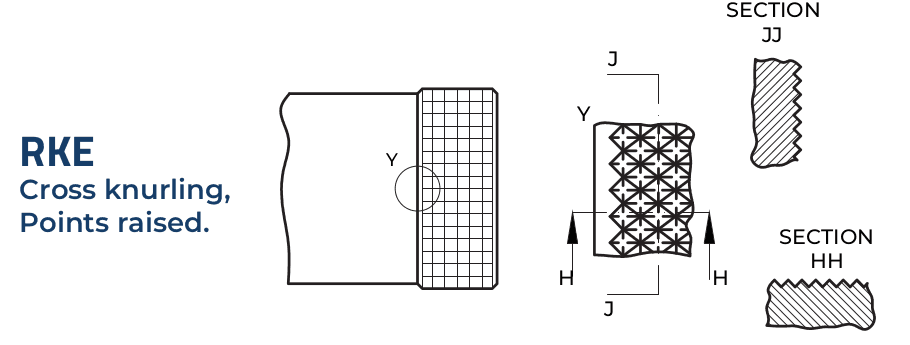
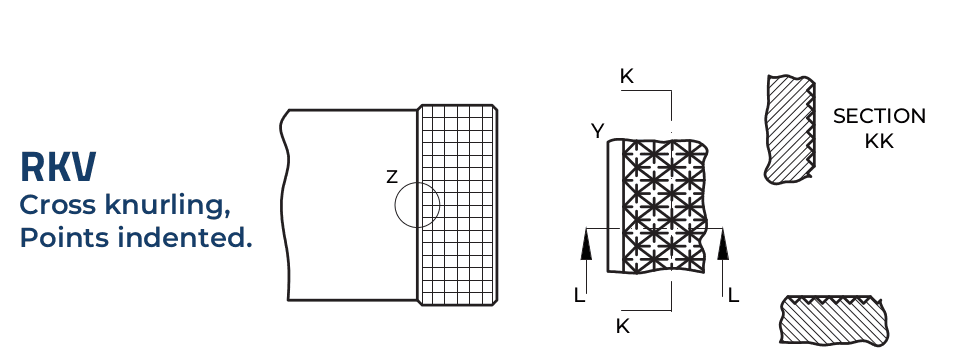
Key Definitions
- Profile Angle: 90° (standard)
- Pitch (P): the circular axial pitch of the knurl
- Nominal Diameter (d1): the outside diameter of the finished knurl, as stated in the workshop drawing; a function of the design
- Initial Diameter (d2): the workpiece diameter before knurling. It is smaller than d1, since the knurling operation enlarges the diameter through displacement of material
Initial Diameter (d2) Formulae
The initial diameter d2 for knurls with a 90° profile angle can be calculated from the table below, depending on the type of knurl and the size of pitch. These formulae don't account for rounding of the grooves from the knurling operation, or the specific properties of the material being knurled.
| Type of Knurl | Initial Diameter d2 |
|---|---|
| RAA: grooves parallel to axis | (no radial displacement) |
| RBL: Left-hand knurl | d1 − 0.5P |
| RBR: Right-hand knurl | d1 − 0.5P |
| RGE: Left/right-hand, points raised | d1 − 0.67P |
| RGV: Left/right-hand, points indented | d1 − 0.33P |
| RKE: Cross-knurl, points raised | d1 − 0.67P |
| RKV: Cross-knurl, points indented | d1 − 0.33P |
Designation example: A cross-knurl, points indented (Type RKV) with pitch P = 0.8mm, conforming to this standard, is designated: Knurl RKV 08 IS:3468